Machine Frame Transforms
Important
NEW FEATURE: Belt printer support
Available in: Nightly builds with the _belt suffix (built from the belt-printer branch) or Releases greater than 2.4.2.
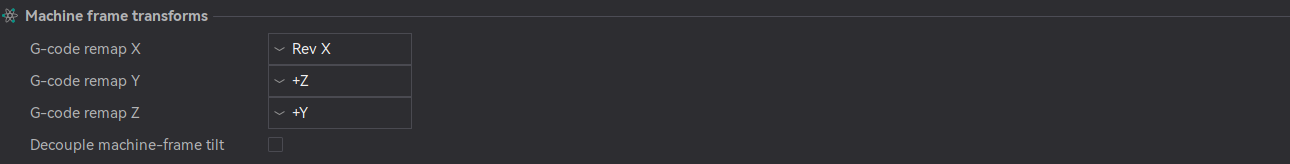
These settings convert OrcaSlicer's coordinates into machine coordinates for a belt printer. They are found in Printer settings → Basic information → Machine frame transforms and are shown when belt printing is enabled. The remap rows are only shown in Developer mode.
The transforms are applied in this order:
- The G-code axis remap determines which slicer axis maps to each machine axis.
- The machine-frame tilt compensates for the gantry not being perpendicular to the belt.
These settings are configured in the printer profile to match the machine's kinematics. The Belt Printing guide explains their role in the slicing process.
Caution
Incorrect values can send the toolhead to an unintended position, potentially beyond the machine's travel limits. Check the result with Show raw G-code (belt only) in the preview's view menu (see Preview), and monitor the first print at the printer.
How axis remapping works
An axis remap has three fields, X, Y and Z, one for each output axis. Each field selects an input axis and defines how its coordinate is mapped to the output. Together, the three fields swap, flip and mirror axes without changing distances.
Remap values
| Value | Result for a coordinate v on the selected input axis |
|---|---|
| +X, +Y, +Z | v: the coordinate is copied. |
| -X, -Y, -Z | -v: the coordinate is negated, so the axis is flipped about the origin. |
| Rev X, Rev Y, Rev Z | max - v: the axis is mirrored inside the build volume, so 0 becomes max and max becomes 0. |
For the Rev values, max is the maximum coordinate of the selected input axis: the largest X or Y coordinate in the printable area, or the printable height for Z.
Leaving the three fields at +X, +Y, +Z preserves the original coordinates.
Example: the belt profiles
The belt profiles included with OrcaSlicer use this G-code axis remap:
| Field | Value | Meaning |
|---|---|---|
| X | Rev X | Machine X runs across the belt, mirrored: X = width - x. |
| Y | +Z | Machine Y, the gantry axis, receives the height above the belt. |
| Z | +Y | Machine Z, the belt axis, receives the position along the belt. |
A point placed in Prepare at x = 20, y = 100, z = 5 on a belt 350 mm wide is therefore remapped to X = 330, Y = 5, Z = 100. The machine-frame tilt is then applied to those coordinates.
Where the remap is applied
The remap acts on the toolpaths after slicing, so it only changes the axis letters and coordinate values used to write each move. The model itself is only rotated by the belt tilt before slicing, and that rotation is undone before the remap, so the remap receives points in the coordinate system of the model as placed in Prepare.
flowchart LR
    A[Model] --> B[Belt tilt rotation]
    B --> C[Slice]
    C --> D[Back-transform]
    D --> E[G-code axis remap]
    E --> F[Machine-frame tilt]
    F --> G[G-code]
What to watch for
- Use every input axis exactly once. OrcaSlicer does not check this. Assigning the same input axis to two outputs, for example +X in both the X and Y fields, discards one axis and flattens the print.
- Custom G-code is not remapped. Start, end, layer change and other machine G-code is written to the file unchanged, so it must already be in machine coordinates.
- Every move is written with X, Y and Z while a remap is active, because any slicer axis can map to any machine axis.
- Arc moves are limited. G2/G3 arcs are only written when X and Y are left at +X and +Y. Arc fitting is disabled on belt printers.
- The remap is stored in the printer profile. The fields are hidden when belt printing is disabled, but any configured remap remains active.
G-code axis remap
Variables: gcode_remap_x, gcode_remap_y, gcode_remap_z.
Type: Choice.
Options: pos_x, pos_y, pos_z, neg_x, neg_y, neg_z, rev_x, rev_y, rev_z.
CLI Example: --gcode-remap-x=pos_x (same pattern for the other variables above).
Selects which slicer axis maps to each machine axis in the exported G-code. The remap is applied during G-code generation, after slicing, and does not change the toolpaths.
The G-code remap X, Y and Z rows are the machine axes. The values are described in How axis remapping works.
These fields are only shown when the settings mode is Developer.
Note
The subsequent machine-frame tilt expects the axis mapping used by the belt profiles: height above the belt on the gantry axis and position along the belt on machine Z.
Machine-frame tilt
Mode: Expert.
Variables: belt_frame_tilt_decouple, belt_frame_tilt_angle.
Type: belt_frame_tilt_decouple (Boolean), belt_frame_tilt_angle (Float).
CLI Example: --belt-frame-tilt-decouple=1 (belt_frame_tilt_decouple shown; other variables above follow their own type).
On a belt printer, the gantry is not perpendicular to the belt. One millimeter of gantry travel therefore raises the nozzle by less than one millimeter and also moves it along the belt. The machine-frame tilt compensates for both effects so that the printed part matches the model.

For a point at height h above the belt and position y along it, with a gantry tilted at angle α:
- The gantry must travel
h / sin αto reach that height. - The layer through the point meets the belt at a distance of
h · cot αfarther along, so the belt position isy + h · cot α.
With the belt profile remap and a belt tilt about X, the remapped coordinates are converted to machine coordinates as follows:
For a belt tilt about Y, the same correction is applied to X instead of Y: X is divided by sin α and Z becomes Z - X · cot α.
For a tilt about X at 45°, this simplifies to Y · 1.414 for the gantry and Z + Y for the belt. At 90°, the gantry is perpendicular to the belt and the coordinates remain unchanged.
By default, the angle is the belt tilt angle, so one value controls both the slicing rotation and this correction. No correction is applied when the tilt axis is Z or None.
Decouple machine-frame tilt
Allows the machine-frame correction to use a separate angle from the belt tilt angle.
Enable this option only when the gantry's physical tilt differs from the slicing angle, for example to slice at 30° on a 45° machine.
Warning
Slicing at an angle different from the gantry's tilt changes how close the nozzle and hotend come to previously printed layers. Check the clearance before printing.
Machine-frame tilt angle
The angle, in degrees, used for the machine-frame correction while Decouple machine-frame tilt is enabled. It is ignored otherwise.